Summary
Common open die forging defects include surface cracks, internal voids, inclusions, laps, cold shuts and improper grain flow. Causes range from incorrect forging temperatures and insufficient deformation to poor ingot quality and flawed heat treatment. Detection methods include ultrasonic testing, magnetic particle inspection and visual examination. Prevention starts with proper ingot selection, controlled forging parameters and experienced process management. For critical applications, third party inspection and full material traceability are essential for forging failure prevention.
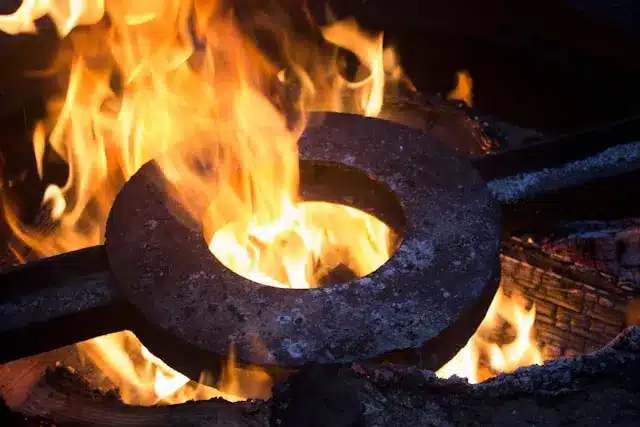
Steel heated to over 1,000 degrees. Pressed under thousands of tons of force. Cooled in water or polymer baths.
A lot can go wrong.
And when it does, the results are expensive. A scrapped forging can cost tens of thousands of euros. Project delays add even more. Reputation damage is harder to measure.
Understanding forging defects helps prevent them. Here is what goes wrong and how to stop it.
Why defects happen in open die forging
Open die forging is not a precise, enclosed process. The steel is shaped between flat or simple dies. The operator controls the process manually. Every blow of the press changes the material.
Temperature fluctuations, uneven deformation and material inconsistencies all create opportunities for defects. Even experienced forges see occasional problems.
The key is knowing what can go wrong. And catching it before the part ships.
Common surface defects
Surface cracks
Surface cracks are among the most common forging defects. They appear as visible lines or tears on the surface.
Causes: Forging at too low a temperature is the primary cause. When steel cools below its optimal forging range, it loses ductility. The surface tears under deformation. Excessive deformation in a single pass can also cause surface cracking. Uneven cooling creates thermal stresses that crack the surface.
Detection: Visual inspection catches many surface cracks. Magnetic particle inspection (MPI) reveals finer cracks that are not visible to the eye. Dye penetrant testing is another option for non-magnetic materials.
Prevention: Maintain the correct forging temperature throughout the process. Reheat the workpiece before it drops below the minimum forging temperature. Use appropriate deformation rates.
Laps and folds
Laps occur when metal folds over during forging. The fold gets pressed into the surface. It looks like a crease that has been flattened.
Causes: Improper die design or positioning. Too much material flowing in one direction during a press stroke. Incorrect sequencing of forging operations.
Detection: Visual inspection and MPI can detect most laps. They appear as linear surface indications, often with oxide scale trapped in the fold.
Prevention: Careful process planning. Experienced operators who control material flow during each press stroke. Proper tooling.
Scale inclusions
Oxide scale forms on hot steel surfaces. During forging, this scale can get pressed into the metal.
Causes: Insufficient descaling before or during forging. Reheat furnace conditions that produce excessive scale.
Detection: Visual inspection after machining. Ultrasonic testing can detect subsurface scale inclusions.
Prevention: Proper descaling between forging operations. Controlled furnace atmospheres.
Common internal defects
Internal voids and porosity
Voids are empty spaces inside the forging. They originate from the ingot casting process.
Causes: The original steel ingot contains shrinkage cavities from solidification. If the forging ratio is too low, these voids do not close completely. The forging process should compress and weld these internal voids shut. But insufficient deformation leaves them open.
Detection: Ultrasonic testing (UT) is the primary detection method. Sound waves reflect off internal voids, showing them on the test display. Full volumetric UT scanning is standard for critical forgings.
Prevention: Use quality ingots from reputable steel mills. Apply sufficient forging ratio to close internal porosity. Minimum forging ratios are typically specified in the relevant standards.
Non-metallic inclusions
Inclusions are particles of non-metallic material trapped in the steel. They originate from the steelmaking process.
Causes: Slag, refractory particles or deoxidation products become trapped during casting. They remain in the steel through forging. Large or clustered inclusions weaken the material.
Detection: Ultrasonic testing reveals larger inclusions. Microscopic examination of test samples shows the type, size and distribution of inclusions.
Prevention: Source steel from mills with strict cleanliness standards. Specify inclusion requirements in the material specification. Higher quality steel grades and vacuum degassing processes reduce inclusion content.
Hydrogen flaking
Hydrogen dissolved in liquid steel can cause internal cracks during cooling. These appear as bright, shiny fracture surfaces called flakes.
Causes: Excessive hydrogen content in the steel. Rapid cooling of large sections traps hydrogen. As the steel cools, hydrogen tries to escape but cannot. The pressure creates internal cracks.
Detection: Ultrasonic testing detects hydrogen flakes. They appear as multiple small, scattered indications.
Prevention: Hydrogen degassing during steelmaking. Slow cooling after forging to allow hydrogen to diffuse out. Some specifications require a hydrogen degassing hold.
Heat treatment related defects
Improper microstructure
Heat treatment transforms the internal structure of the steel. Done wrong, it creates problems.
Scenario: A forged duplex stainless steel ring undergoes heat treatment. The cooling rate is too slow. Sigma phase forms in the microstructure. This destroys impact toughness and corrosion resistance. The entire forging may need re-heat treatment. If the damage is too severe, it is scrap.
Causes: Wrong temperature. Wrong holding time. Wrong cooling rate. Each steel grade has specific parameters. Missing any of them produces the wrong microstructure.
Detection: Mechanical testing reveals the effects. Impact tests show low toughness. Hardness tests show unexpected values. Metallographic examination confirms the microstructure.
Prevention: Follow the heat treatment procedure for the specific steel grade. Use calibrated furnaces and cooling systems. For critical grades like duplex and superduplex, only experienced heat treatment facilities should be used.
Quench cracking
Rapid cooling during quenching creates thermal stresses. If these exceed the material’s strength, cracks form.
Causes: Too aggressive quenching medium for the component geometry. Sharp corners or sudden section changes concentrate stress. Large temperature differences between surface and core.
Detection: MPI and UT after quenching. Quench cracks often appear at stress concentration points like corners, fillets and cross-section changes.
Prevention: Select the appropriate quenching medium (water, oil or polymer) for the steel grade and geometry. Avoid sharp corners in the forging design. Control quench parameters carefully.
Distortion
Heat treatment can cause the forging to change shape. Rings can become oval. Flat surfaces can warp.
Causes: Uneven heating or cooling. Asymmetric cross sections. Residual stresses from forging.
Detection: Dimensional measurement after heat treatment. Ovality checks on rings. Flatness checks on discs.
Prevention: Uniform heating and cooling. Proper support during heat treatment. For critical parts, a stress relief treatment before the main heat treatment can help. Post-heat treatment straightening may be possible for some geometries.
Machining related issues
Distortion during machining
Even after successful forging and heat treatment, problems can appear during machining.
Residual stresses hide inside the forging. Machining removes material and redistributes those stresses. The part can shift, warp or spring open.
Scenario: A large forged block arrives at the machine shop. The machinist cuts it in half for two smaller parts. The halves spring apart. Internal stresses from inadequate stress relief cause the distortion. The parts are now out of tolerance.
Causes: Insufficient stress relief before machining. Removing too much material in one pass. Asymmetric material removal.
Prevention: Stress relieve the forging before precision machining. Remove material symmetrically. Allow for roughing and finishing passes with stress relief in between for critical tolerances.
Tool failure from unexpected hardness
Incorrect heat treatment can leave areas of unexpected hardness. Machining tools break or wear prematurely.
Prevention: Verify hardness at multiple locations before machining. Ensure heat treatment was performed correctly.
The role of inspection and testing
Non-destructive testing (NDT)
NDT is the safety net. It catches defects before they reach the end client.
Ultrasonic testing (UT) checks the full volume of the forging. It finds internal voids, inclusions, cracks and flakes.
Magnetic particle inspection (MPI) checks surfaces for cracks and laps. It is sensitive to very fine surface breaking defects.
Dye penetrant inspection (DPT) is similar to MPI but works on non-magnetic materials like austenitic and duplex stainless steels.
Mechanical testing
Tensile testing, impact testing and hardness testing verify that the material meets specification. Results outside the acceptable range indicate a problem with the forging or heat treatment process.
Third party inspection
For certified projects, an independent inspector witnesses testing. This provides an additional layer of verification. Inspectors from organisations like Lloyd’s, DNV or Bureau Veritas ensure objectivity.
How to prevent forging defects
Start with good material
Ingot quality sets the ceiling for forging quality. Poor steel produces poor forgings. Specify clean steel with low inclusion content. Source from reputable mills.
Choose the right forge
An experienced forge knows how to manage the process. Temperature control, deformation sequence and cooling all require skill. Forges that specialise in your material grade and component type reduce risk.
Specify the right heat treatment
Match the heat treatment to the steel grade and the application. Ensure the forge or heat treatment facility has experience with your specific material. For duplex steels, this is especially critical.
Inspect at every stage
Do not wait until the end to test. Check the ingot. Inspect after forging. Test after heat treatment. Verify after machining. Each checkpoint catches problems earlier, when they are cheaper to address.
Work with an experienced supply chain partner
Coordinating forging, heat treatment, machining and inspection across multiple facilities creates handover risks. A supply partner who manages the full chain reduces those risks. They know what to watch for at each stage.
Frequently asked questions
What is the most common open die forging defect?
Surface cracking from incorrect forging temperature is among the most common defects. Internal defects like voids and inclusions from poor ingot quality are also frequently encountered.
How are internal forging defects detected?
Ultrasonic testing (UT) is the primary method for detecting internal defects. Sound waves travel through the steel. Any internal discontinuity reflects the sound back. The size, location and nature of defects can be characterised from the UT response.
Can forging defects be repaired?
Some surface defects can be ground out if they are shallow and the remaining wall thickness still meets requirements. Internal defects generally cannot be repaired. Re-heat treatment can sometimes correct microstructure problems. But cracks, voids and inclusions typically mean the forging is scrapped.
What is the cost of a scrapped forging?
Costs vary widely depending on size, material grade and stage of production. A large forging in duplex or superduplex steel can represent a significant investment. If the defect is found after machining, both the forging cost and the machining cost are lost. Project delays add further costs.
How does forging ratio affect defect risk?
A higher forging ratio means more deformation. More deformation closes internal voids better. It refines the grain structure more thoroughly. Low forging ratios leave residual porosity and coarser grains. Minimum forging ratios are typically specified for critical applications.
What certifications help ensure forging quality?
NORSOK M-650 qualification ensures the manufacturer can consistently produce special alloy forgings. EN 10204 3.2 certificates provide third party verification of material properties. ISO 9001 or similar quality management systems document process controls.